
Optical Frame
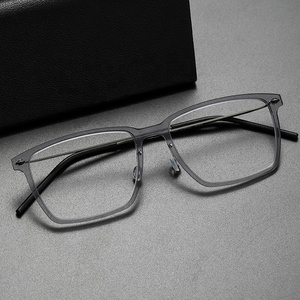
Unisex Ergonomic
Spring Hinge
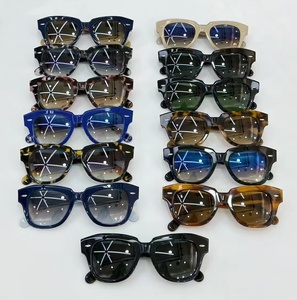
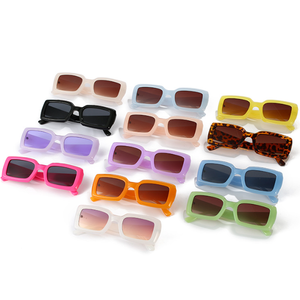
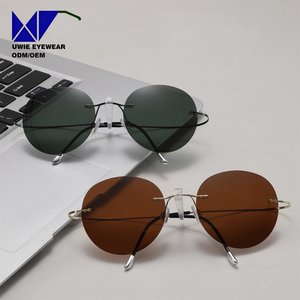
Direct-from-manufacturer private label solutions spanning Mazzucchelli-grade acetate, aerospace beta-titanium, polarized sun optics, and medical-grade precision assemblies.
A technical assessment of next-generation optical fabrication, sustainable polymer chemistry, and automated tolerance standards defining competitive export supply chains.
The global luxury and mid-market eyewear segments are undergoing a fundamental structural transition toward environmental compliance and circularity. Traditional cellulose acetate, while derived from natural cotton linters and wood pulp, has historically relied on fossil-fuel-based diethyl phthalate (DEP) plasticizers. As independent optometry chains and international fashion conglomerates face heightened corporate sustainability directives, Chinese Tier-1 eyewear original equipment manufacturers (OEMs) have engineered proprietary Bio-Cellulose Acetate formulations.
These bio-acetates replace petroleum plasticizers with triethyl citrate and vegetable-derived additives, achieving biodegradation metrics exceeding ISO 14855 standards (over 90% degradation within 180 days under industrial composting conditions) without sacrificing tensile strength, surface luster, or thermodynamic adjustability. Concurrently, zero-waste closed-loop systems have been integrated into high-speed CNC milling lines. Sintered acetate shavings generated during temple profiling and eye-wire shaping are vacuum-harvested, dissolved in non-toxic solvents, re-granulated, and calendered into recycled acetate sheets (RPET and R-Acetate collections), yielding a measurable 42% carbon footprint reduction per manufactured unit.
Technical Specification Metric: Premium bio-based cellulose acetate exhibits a flexural modulus of 2,200–2,600 MPa and an equilibrium moisture absorption of <1.8%, preventing structural warping during long-term maritime transit and high-humidity display conditions.
Metal frame manufacturing in specialized Chinese optical hubs (notably Shenzhen's Henggang and Wenzhou's Ouhai clusters) has pivoted rapidly from standard nickel-silver and basic Monel alloys to ultra-pure Grade 5 (Ti-6Al-4V) and Beta-Titanium (Ti-15V-3Cr-3Sn-3Al). Beta-titanium offers superior elasticity, exceptional shape-memory characteristics, and complete bio-compatibility, eliminating skin contact allergies governed under EU REACH and EN 16128 nickel-release directives.
The manufacturing complexity of titanium frames hinges on its reactivity with oxygen at elevated temperatures. Modern export manufacturers utilize automated multi-axis fiber laser micro-welding stations sealed in high-purity argon chambers (>99.999% Ar). This inert-gas shielding eliminates atmospheric embrittlement and micro-cracking across bridge-to-rim joints and temple hinge mounts, increasing mechanical joint tensile resistance beyond 450 N. Furthermore, physical vapor deposition (PVD) vacuum ion-plating coats these substrates with titanium nitride (TiN) or diamond-like carbon (DLC) layers down to 0.8–1.2 microns, ensuring salt-spray corrosion resistance that surpasses 96-hour continuous fog testing (ASTM B117).
Modern acetate production utilizes 5-axis synchronous German and Japanese CNC routers. Operating at spindle speeds up to 24,000 RPM with diamond-tipped tooling, frames maintain internal lens groove dimensions within a ±0.02mm tolerance, preventing prescription lens pop-out and stress cracking during automated edging.
Frames undergo a 72-hour, 4-stage automated rotary barrel polishing process utilizing calibrated beechwood chips, birch granules, and micro-fine pumice paste. This is finalized with hand-buffing using carnauba wax to produce a mirror-grade finish with zero orange-peel micro-defects.
Integrating electronics into private-label eyewear demands modular IP67-rated architectural cavity tooling. Precision-molded TR90 temples now feature hollowed channels for directional acoustic micro-speakers, dual beamforming microphones, and magnetic pogo-pin charging interfaces.
How international eyewear brands, clinic chains, and volume distributors optimize lead times, mitigate tariff volatility, and execute agile inventory replenishment.
The conventional private-label paradigm—demanding rigid minimum order quantities (MOQs) of 1,200 pieces per acetate model across four fixed colorways—has been made obsolete by decentralized consumer demand and hyper-targeted DTC brand launches. Progressive Chinese manufacturers and export distributors now deploy an Agile Semi-Finished Inventory Model (ASIM).
Under this operational structure, primary chassis (front rims and standardized core-wire temples) are CNC-profiled and tumbled in volume batches of 3,000 to 5,000 units in unpolished transparent or black base materials. Brand buyers can then issue dynamic purchase orders as low as 100 to 300 pieces per SKU for localized custom laser branding, custom color dip-dyeing, physical vapor deposition (PVD) detailing, or specific prescription demo lens fitting. This mechanism shortens product iteration cycles from 90 days down to 14 business days, freeing working capital and preventing dead-stock write-downs.
Photopolymer resin SLA and Selective Laser Sintering (SLS) nylon printing generate functional fit-verification samples within 72 hours, eliminating the need for expensive pilot steel mold cutting.
Custom hydraulic stamping of decorative nickel-silver and brass inner core wires provides bespoke brand aesthetics visible through crystalline acetate temple bodies.
High-resolution telecentric optical vision systems verify four-point frame symmetry, temple splay angles, pantoscopic tilt (8°–12°), and bridge groove continuity in real time.
End-to-end customs clearance handling under HS Codes 9003.11 (plastics) and 9003.19 (other materials), coordinating tariff mitigation with air and sea multimodal delivery.
Export-ready frames built in accordance with international medical and optical regulations, including ISO 12870, ANSI Z80.3, and FDA 21 CFR 801.410 impact resistance.
A reputable China eyewear manufacturer must prove sustained compliance across strict physical, optical, and chemical vectors. Every export consignment destined for European, North American, or Asia-Pacific markets undergoes exhaustive pre-shipment laboratory batch testing:
Automated mechanical actuators flex frame temples through a continuous 20,000-cycle open-close sequence at 40 cycles/minute. Zero screw back-out or hinge play greater than 0.5° is permitted.
Subjected to static 50N downward loading across the nasal bridge to evaluate elastic recovery and structural memory, guaranteeing frames retain their optical base curve without lens detachment.
Frames endure 24 hours of simulated human perspiration immersion followed by exposure to 60°C dry heat and 95% relative humidity for 48 hours to confirm zero surface bubbling or discoloration.
In accordance with FDA 21 CFR 801.410, a 5/8-inch steel ball weighing approximately 0.56 ounces is dropped from a height of 50 inches onto sun and demo lenses to confirm zero structural fracture.
Bridging aesthetic conceptualization with scalable industrial precision through structured OEM/ODM execution milestones.
Converting 2D designer sketches into 3D parametric CAD files (IGES/STEP). Calculating precise facial pantoscopic angle, nasal bridge contouring, and temple wrap parameters.
Fabrication of hardened steel stamping dies, hinge placement jigs, and CNC cutter toolpaths. Functional physical prototypes delivered for optician fitting evaluation.
High-precision multi-axis frame profile routing, custom core-wire hydraulic shooting, robotic hinge staking, and consecutive three-stage barrel abrasive polishing.
Ion PVD plating, electrostatic color spraying, pad printing, high-resolution laser micro-engraving, and custom eco-friendly packaging integration.
Actionable answers covering technical tolerances, tooling investments, custom branding options, and international shipping protocols.